


What Causes RO Antiscalants to Fail at Higher Recovery Rates? (And How to Prevent It)
What Causes RO Antiscalants to Fail at Higher Recovery Rates? (And How to Prevent It)
Raising reverse osmosis recovery reduces concentrate discharge, but it also narrows the operating margin for scale control. A treatment program that worked at lower recovery may become unreliable as dissolved salts concentrate, membrane-surface conditions change, and small dosing problems become harder to tolerate.
The answer is not automatically more antiscalant. Operators and formulators need to establish which mineral is approaching its limit, whether the chemical is reaching the membrane consistently, and whether the proposed recovery is realistic for the water chemistry and system design.
Higher recovery changes conditions more than the percentage suggests
For a highly rejected dissolved salt, a useful first approximation is:
Concentrate concentration factor ≈ 1 ÷ (1 − recovery)
At 75% recovery, this factor is approximately four. At 85%, it is about 6.7. That apparently modest recovery increase therefore raises the theoretical concentrate salt level by roughly two-thirds. These are mass-balance estimates, not design limits: salt passage, precipitation, recycle arrangements, and staging affect actual conditions.
The membrane surface can experience still higher concentrations because of concentration polarization. Tail-end elements are particularly exposed as salts accumulate and concentrate flow declines. If an operator increases recovery mainly by restricting concentrate flow, inadequate crossflow can compound the chemical risk.
Antiscalants delay crystal nucleation and growth; they do not remove the dissolved salts. Their protection has limits, and those limits depend on the mineral, formulation, temperature, pH, and time available for precipitation.
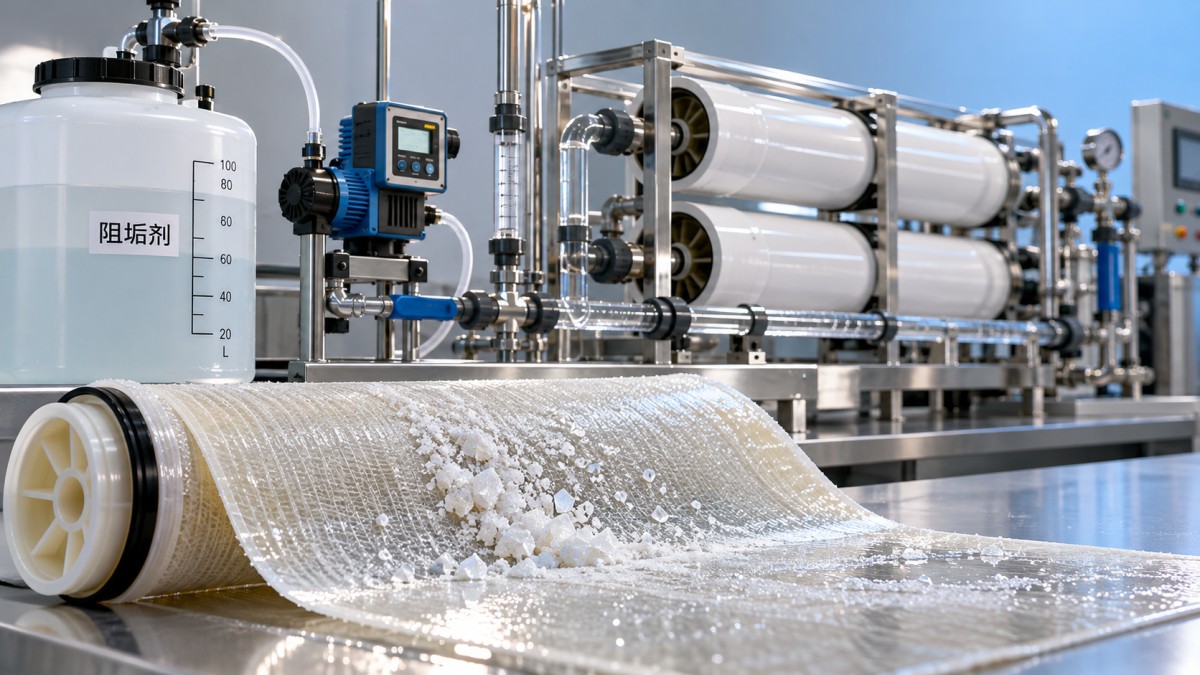
The controlling scale may no longer be calcium carbonate
A frequent mistake is carrying the original antiscalant selection into a higher-recovery operating plan without checking which mineral now controls the limit. Good calcium carbonate inhibition does not establish adequate protection against calcium sulfate, barium sulfate, strontium sulfate, or silica deposition.
Barium and strontium deserve attention even when their feed concentrations appear small. Silica requires a different assessment from carbonate scale, particularly when aluminum or iron carryover is present. A carbonate-focused saturation index alone cannot describe these risks.
Request a current analysis covering calcium, magnesium, alkalinity, sulfate, silica, barium, strontium, iron, aluminum, pH, temperature, and the major ions needed for a credible ionic balance. For wastewater reuse, include relevant phosphate and pretreatment residuals. Model the intended operating envelope—not just an average sample collected months earlier.
Acid adjustment may reduce carbonate scaling potential, but it does not solve every mineral problem. Sulfuric acid also adds sulfate, which can be an unfavorable trade where sulfate scales already constrain recovery.
A running dosing pump does not prove adequate treatment
Higher recovery often exposes delivery faults that previously went unnoticed. A partly blocked injection valve, loss of pump prime, incorrect dilution, or a deteriorating check valve can leave the system underdosed while the control screen still shows normal operation.
Check chemical delivery by measurement rather than pump setting alone:
- Verify actual pump output against the current feed flow and specified product dosage.
- Confirm whether the dosage is expressed as supplied product or active material; these are not interchangeable.
- Check dilution-water quality, solution age, tank cleanliness, and the supplier’s dilution instructions.
- Confirm that injection provides adequate mixing and starts before untreated water reaches the membranes.
More chemical is not an unlimited safety margin. Excessive dosage may increase cost without extending the validated inhibition range, and some formulations can contribute to deposits or interactions under unfavorable conditions. Any increase should remain within a technically supported application range.
Compatibility problems can look like antiscalant failure
Residual cationic coagulants can interact with anionic antiscalants and form foulants. Iron and aluminum carryover may also promote mixed deposits. Under those conditions, changing antiscalant brands without correcting pretreatment can leave the underlying problem untouched.
Likewise, a dispersant raw material should not be treated as a finished RO antiscalant simply because it controls calcium carbonate in another application. For example, Sodium of Maleic Acid and Acrylic Acid Copolymer Dispersant (MA-AA·Na) is a phosphorus-free polymer with chelating and dispersing properties, supplied for applications including detergents, textiles, coatings, and slurries. Those properties may interest formulators, but they do not establish suitability for high-recovery RO.
Any proposed RO use needs application-specific evidence covering molecular characteristics, impurities, calcium tolerance, membrane compatibility, and inhibition of the relevant scale. Solids content alone cannot predict performance. The same caution applies when substituting apparently similar polymer grades in an established formula.
For a raw-material and formulation supplier such as Prio New Materials, the useful technical discussion starts with the water analysis and operating target. Its combination of polycarboxylate dispersants, organophosphorus materials, customized formulation development, and laboratory support provides a basis for evaluation—not a reason to skip compatibility testing.
Confirm the deposit before changing the chemistry
Declining permeate flow does not, by itself, prove scaling. Biofouling, colloidal material, organic deposits, temperature changes, and membrane damage can produce overlapping symptoms. Track normalized permeate flow, normalized salt passage, and stage differential pressure alongside feed, permeate, and concentrate measurements.
A tail-end performance problem is consistent with concentration-related scaling, while a rising lead-stage pressure drop often directs attention toward incoming foulants. Neither pattern is a diagnosis. Deposit analysis, cartridge-filter inspection, and, where justified, membrane autopsy provide stronger evidence than appearance alone.
If scale is already established, simply increasing antiscalant will not reliably remove it. Use a deposit-specific cleaning procedure approved for the membrane, then address the cause before restoring the higher recovery.
Raise recovery through a controlled operating trial
Before making a permanent change, establish a stable baseline, verify dosing, and complete a scale projection using current water chemistry. Confirm membrane-vendor limits for element recovery, flux, and minimum concentrate flow. Then increase recovery in controlled steps, with agreed monitoring intervals and rollback criteria.
A short period without visible deposits is not proof of long-term protection. Watch normalized trends and account for seasonal temperature shifts, feed blending, and pretreatment changes. Where the projected chemistry exceeds a formulation’s supported range, consider softening, selective ion removal, revised staging, or lower recovery rather than repeatedly escalating dosage.
The practical target is not the highest recovery the plant can reach today. It is the recovery it can hold through feedwater variation without accelerating deposition, cleaning frequency, or membrane deterioration.

ONLINE CONSULTATION
If you have any questions, please contact us and we will contact you as soon as possible.